Thanks to Chad Kelly, Isaiah Schroeder, and mflgrmp for becoming Knife Steel Nerds Patreon supporters!
Background Information and CATRA Curves
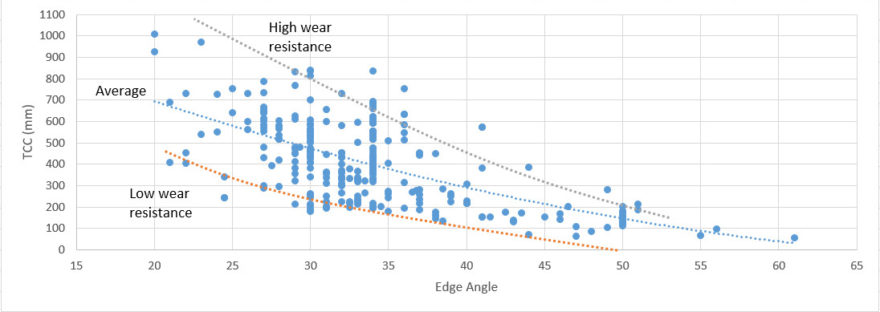
Make sure you read Part 1 first so that you understand all of the background information for this article.
Below I have another Youtube video of CATRA testing so that you can see how the curves are generated during testing.
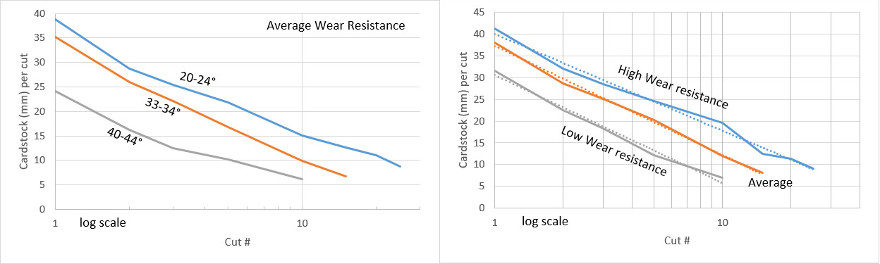
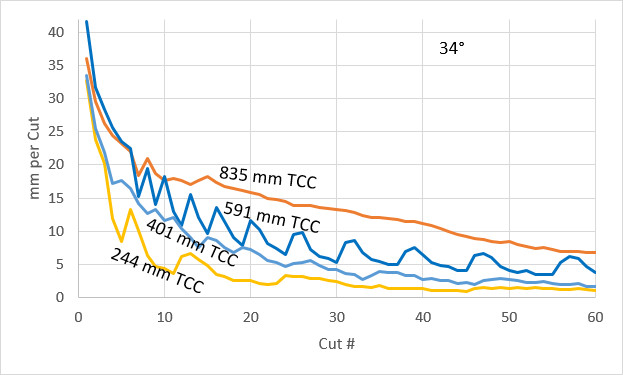
You can get a feel for how differently these steels cut by plotting a few of them together with the same edge angle. The top curve is a high wear resistance steel which cut 835 mm of cardstock after 60 cuts, which is the TCC value (Total Cardstock Cut). The 244 mm is a medium-low wear resistance steel which shows much more sharpness loss than the higher wear resistance steels.
Edge Radius During the CATRA Test
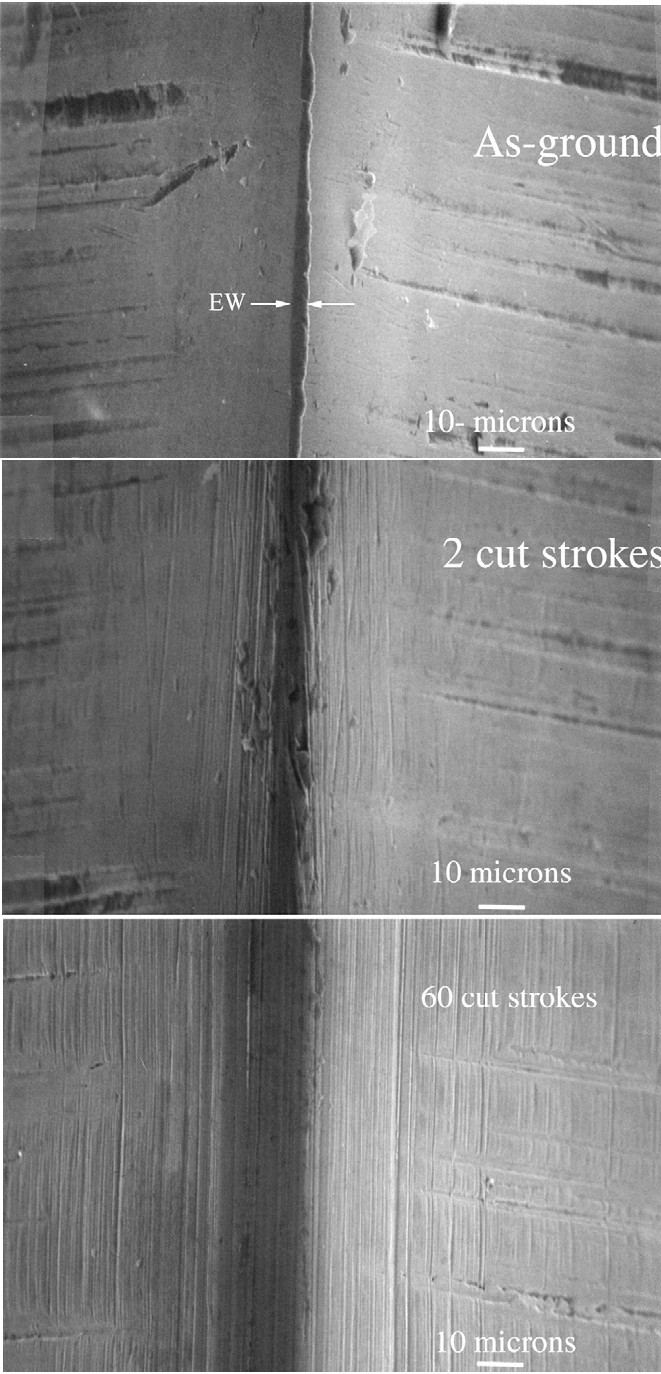
I’m not sure where in the test the average person would decide that the knife needs to be resharpened, but I would guess that it is before cut 60 because the CATRA test wears the edge pretty significantly. In CATRA tests performed by Verhoeven [1] the edge radius was reduced from ~0.5 micron all the way to 3-5 microns after only the second cycle (note he calls the cycles strokes):
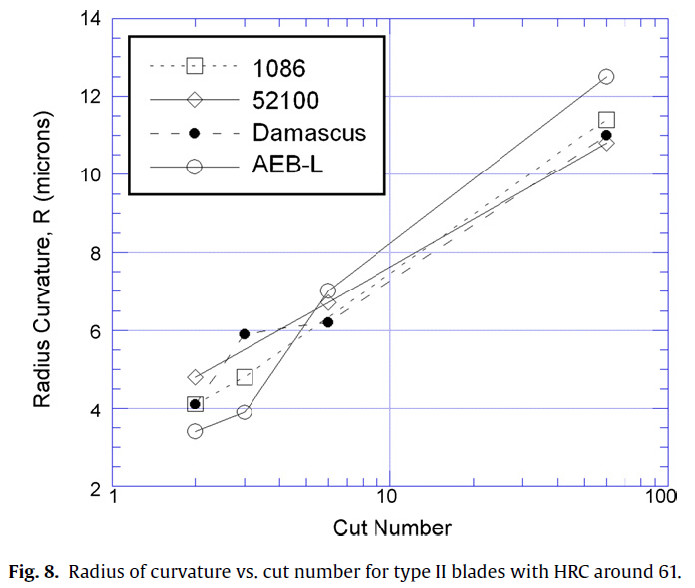
The tests performed by Verhoeven were with low wear resistance steels (AEB-L, 52100, 1086, and Wootz) but it still shows the relatively significant wear that occurs with the CATRA test. In the CATRA article on 154CM, it was found that the edge width (rather than radius measured by Verhoeven) was increased to 23 microns with a 20° edge angle and the 50° edge to 17 microns, which is quite dull. A ten micron edge width has been reported previously as a dull edge that needs sharpening [2].
Regression Factors Analysis
In part 1 I described the process by which we calculated the relative factors that affect edge retention which resulted in the equation below. CrC is a general term to refer to either Cr7C3 or Cr23C6 chromium carbides. CrVC is a general term to refer to M7C3 where M can be either Cr or V; when vanadium is added to a high chromium steel the chromium carbides are enriched with vanadium which increases the hardness of the Cr carbides. MC can refer to either vanadium carbides (VC) or niobium carbides (NbC). MN can refer to either vanadium nitrides (VN) or niobium nitrides (NbN). CrN refers to chromium nitrides. The formation of these particles is controlled primarily by the composition of the steel and secondarily by processing and heat treating. The equation below and the tables in Part 1 and here in Part 2 come from journal articles and books that have reported the carbide fractions after heat treatment.
TCC (mm) = -157 + 15.8*Hardness (Rc) – 17.8*EdgeAngle(°) + 11.2*CrC(%) + 14.6*CrVC(%) + 26.2*MC(%) + 9.5*M6C(%) + 20.9*MN(%) + 19.4*CrN(%)
Carbide Hardness
Taking an average value of the hardness of each carbide type we can compare between carbide hardness [3][4] and the calculated coefficient. Below I have plotted the carbide hardness in vickers (Hv) on the x-axis vs our calculated coefficient in the equation above for the relative contribution to edge retention for each carbide type. We get a very good correlation, demonstrating that carbide hardness strongly controls the effect of a carbide on slicing edge retention:
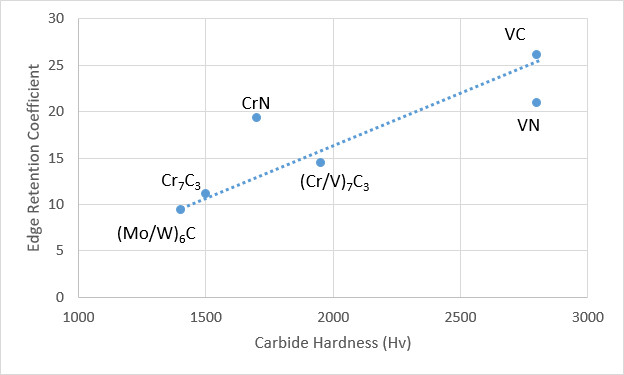
The coefficient for VC (listed as MC in the equation) is somewhat higher than the nitrogen version (VN or MN) despite their reported similar hardness [4]. Either the VN is actually somewhat softer or this is due to the VN coefficient being based on only two CATRA tests on one steel (Vanax 35). Either way it appears to be qualitatively accurate. Another possibility is that there may be some formation of V2N or chromium carbide/nitride which is lower in hardness than VN. The value for CrN also falls off the trend line of the others but that value comes from only one steel, Cronidur 30, and would likely change if further tests were performed. The M6C value is based on only two steels, CPM-M4 and M2, which both get wear resistance from VC so the accuracy of the M6C coefficient could definitely be improved with other high speed steels. No simple carbon steels with Fe3C cementite were tested which would be nice to add to the regression. Due to the low hardness of cementite it would be expected to have a relatively low value. This is confirmed by the Verhoeven study comparing 52100, 1086, and AEB-L where AEB-L with chromium carbides had superior edge retention to 52100 and 1086 with cementite [1]. If we extend the trendline in the plot above to the hardness of cementite we would estimate a coefficient of 5, or about half of chromium carbide. Experiments would be necessary to confirm that. Another interesting set of tests would be on the low-alloy tungsten steels such as the Blue series, V-Toku series, F2, O7, etc. The tungsten carbides in those steels are reported to be the very hard WC so it would be nice to know if that carbide improves edge retention to the same extent as VC. They are relatively niche steels so they have not received as much study as many tool steels and stainless steels. I wrote about these low-alloy tungsten steels
in an earlier article on this site read more